
How do I transfer glass bottles between packaging machines?
Practical guidance for glass bottles: coordinate product flow, controls, accumulation, guarding and restart behaviour.
Direct answer
For glass bottles, design the line as one process with agreed speeds, signals, buffers and fault behaviour. A pack must remain clean, stable and correctly orientated through every transfer, filling, closing, labelling and inspection stage. First, create a scaled layout and process sequence and record damage rate, jam rate, position repeatability and finished-pack integrity. Make one controlled change at a time so the original cause is not hidden by several new settings.
Blocked, starved and handshake states
Record each machine’s ready, run, blocked, starved and fault conditions. Check what happens during short stops and restart, not only continuous running.
Application measure: For container and pack handling, include dimensional variation, base stability, guide contact, scuffing, transfer gaps and damage rate.
Packaging Machines UK
See the machinery and application options most closely matched to this production question.
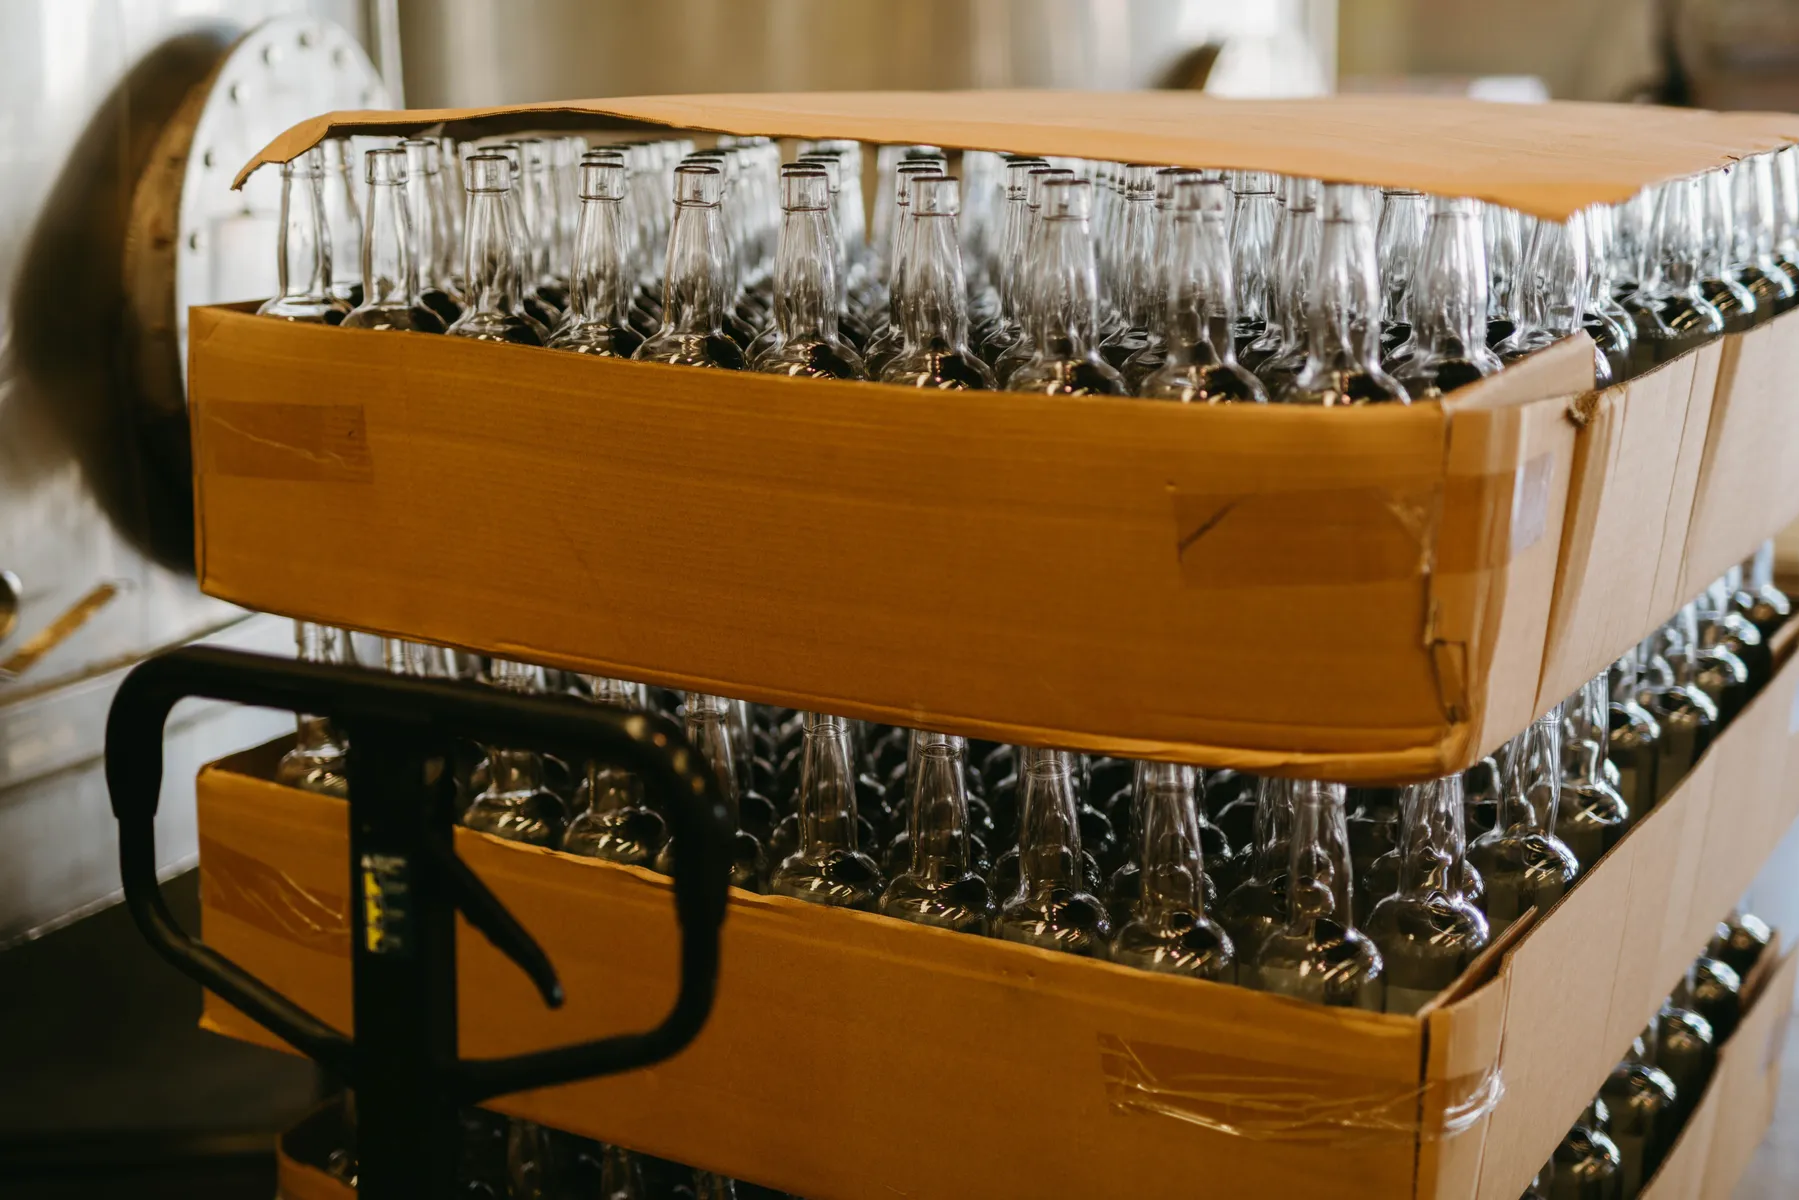
What usually causes this?
- machines selected independently at different heights or effective rates
- A change in dimensional and material variation or base stability and centre of gravity.
- start, stop, ready and fault signals not agreed
- The equipment or handling method not being set for rigid but breakable containers requiring controlled contact and base support.
- no accumulation for normal micro-stops
Checks to make in order
- Create a scaled layout and process sequence
- Record damage rate, jam rate, position repeatability and finished-pack integrity using a representative sample.
- Set one sustained line-rate target
- Check neck, opening or sealing geometry, surface condition and static and guides, transfers and pack support.
- Document electrical and control interfaces
- Calculate accumulation needed for normal stops
- Review access, cleaning, maintenance and restart behaviour
How to decide the next step
Glass bottles involves rigid but breakable containers requiring controlled contact and base support. Use line integration when several machines must operate as one controlled process rather than a row of separate units.
If adjustment and maintenance cannot hold the required result across the complete product and pack range, compare the machinery route against a written acceptance test. The important comparison is sustained good output—not only maximum cycle speed.
What to include in your production brief
Supplying the information below makes it much easier to distinguish a setup problem from a machinery or packaging limitation:
- Dimensioned pack drawing
- Minimum and maximum pack samples
- Material and supplier specification
- Closure or seal components
- Required orientation and label area
- Target line rate
- Samples that represent glass bottles
- A short video of the current process and fault
Relevant solution websites
These specialist sites match the production process discussed above. Final suitability should be confirmed with samples, output, site and acceptance information.
Related questions
 Pack formats
How do I improve the appearance and consistency of glass bottles?
Practical guidance for glass bottles: improve appearance, seal, closure, code, dose and transport performance.
Read the answer → Pack formats
How do I reduce repeated line faults caused by glass bottles?
Practical guidance for glass bottles: turn recurring faults into controlled inspection, service and replacement actions.
Read the answer → Pack formats
How do I feed empty glass bottles automatically?
Practical guidance for glass bottles: present products, packs, caps or components consistently to the next operation.
Read the answer → Pack formats
How do I transfer round bottles between packaging machines?
Practical guidance for round bottles: coordinate product flow, controls, accumulation, guarding and restart behaviour.
Read the answer → Pack formats
How do I transfer square bottles between packaging machines?
Practical guidance for square bottles: coordinate product flow, controls, accumulation, guarding and restart behaviour.
Read the answer → Pack formats
How do I transfer oval bottles between packaging machines?
Practical guidance for oval bottles: coordinate product flow, controls, accumulation, guarding and restart behaviour.
Read the answer →