
How do I automate product handling around print-and-apply labelling?
Practical guidance for print-and-apply labelling: automate the limiting operation without creating a new bottleneck.
Direct answer
For print-and-apply labelling, automate the task that limits output, quality or labour efficiency first. End-of-line equipment must receive stable products at a controlled rate and create a pack that survives handling, storage and transport. First, map the current process and operator movements and record good packs per minute, material use, seal or closure quality and transport damage. Make one controlled change at a time so the original cause is not hidden by several new settings.
Operator touch time and constraint
Time manual handling, waiting and correction separately. Automation should remove a measured constraint or risk; automating a non-bottleneck can move the problem downstream.
Application measure: For end-of-line packing, include pack pattern, material use, seal or tape quality, heat profile, case stability and transport damage.
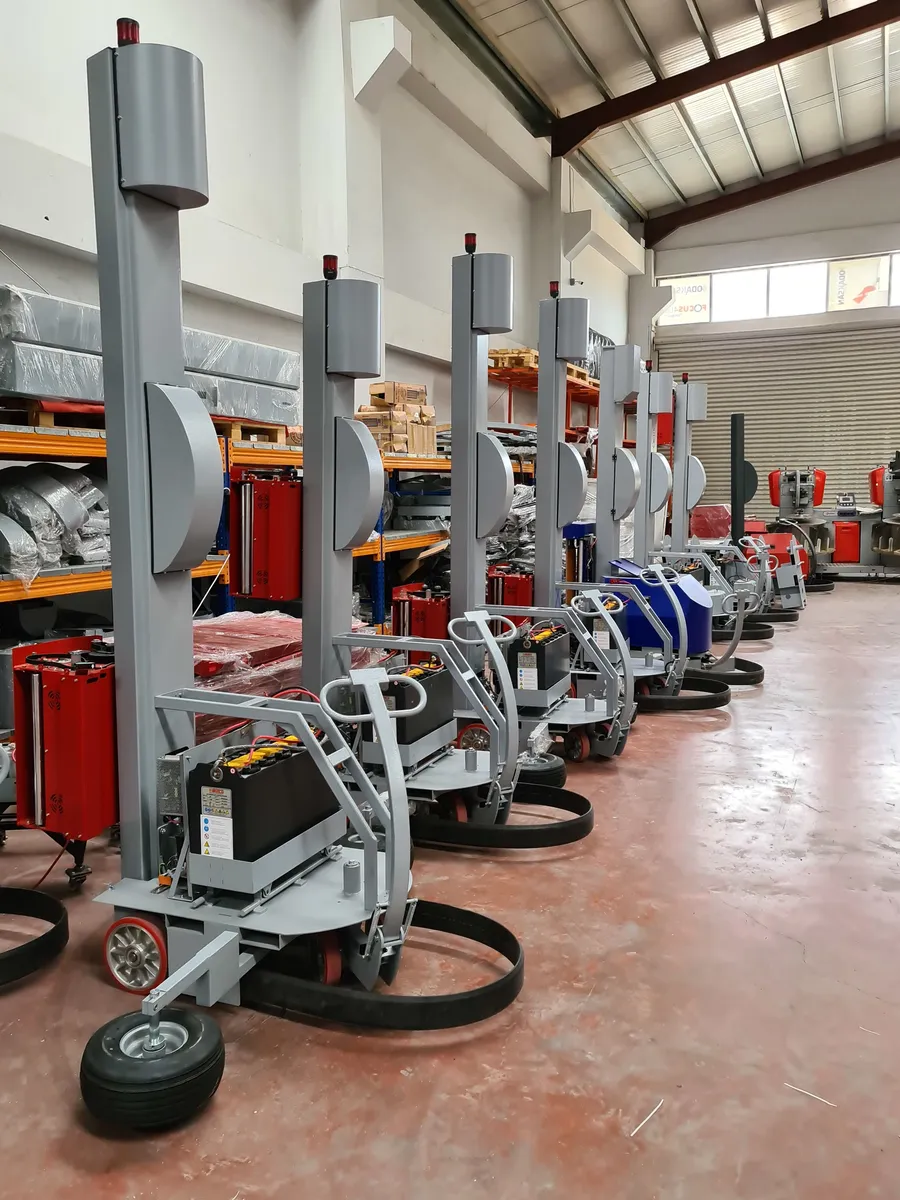
Print and Apply
See the machinery and application options most closely matched to this production question.
What usually causes this?
- a fast machine being added while loading or downstream packing stays manual
- A change in product grouping and spacing or film, carton, case or tray quality.
- insufficient buffers between processes with different stop patterns
- The equipment or handling method not being set for printing variable data and automatically applying it to a moving pack.
- the product or packaging not being presented consistently
Checks to make in order
- Map the current process and operator movements
- Record good packs per minute, material use, seal or closure quality and transport damage using a representative sample.
- Measure cycle time, waiting, rejects and replenishment
- Check machine entry and transfer control, heat, tape, glue or closure settings and finished-pack inspection and discharge.
- Identify the constrained step and the next likely constraint
- Compare one-step, cell and full-line automation
- Include changeover, cleaning, guarding and support in the return calculation
How to decide the next step
Print-and-apply labelling involves printing variable data and automatically applying it to a moving pack. Phase automation where practical, but design interfaces so later machines can be added without rebuilding the line.
If adjustment and maintenance cannot hold the required result across the complete product and pack range, compare the machinery route against a written acceptance test. The important comparison is sustained good output—not only maximum cycle speed.
What to include in your production brief
Supplying the information below makes it much easier to distinguish a setup problem from a machinery or packaging limitation:
- Product and finished-pack dimensions
- Pack pattern and orientation
- Film, board, tape or case specification
- Required output
- Conveyor height and direction
- Transport and stacking test
- Samples that represent print-and-apply labelling
- A short video of the current process and fault
Relevant solution websites
These specialist sites match the production process discussed above. Final suitability should be confirmed with samples, output, site and acceptance information.
Related questions
 End of line
How do I operate print-and-apply labelling safely?
Practical guidance for print-and-apply labelling: control product, machinery, operator and site hazards through competent assessment.
Read the answer → End of line
Which machine is best for print-and-apply labelling?
Practical guidance for print-and-apply labelling: match the machine principle to the real product, pack, output and acceptance criteria.
Read the answer → End of line
How do I prevent repeated faults during print-and-apply labelling?
Practical guidance for print-and-apply labelling: turn recurring faults into controlled inspection, service and replacement actions.
Read the answer → End of line
How do I automate product handling around case taping?
Practical guidance for case taping: automate the limiting operation without creating a new bottleneck.
Read the answer → End of line
How do I automate product handling around cartoning?
Practical guidance for cartoning: automate the limiting operation without creating a new bottleneck.
Read the answer → End of line
How do I automate product handling around shrink wrapping?
Practical guidance for shrink wrapping: automate the limiting operation without creating a new bottleneck.
Read the answer →