
How do temperature and room conditions affect filling mayonnaise?
Practical guidance for mayonnaise: understand how the production environment changes product and machine behaviour.
Direct answer
For mayonnaise, record conditions beside the process before changing several settings at once. This is a filling application where viscosity, aeration, temperature, supply conditions, nozzle control and product-contact compatibility affect dose and pack quality for mayonnaise. Product temperature, positive displacement, large product paths and clean nozzle shut-off are usually important. Use representative product and packaging, keep the order of results and identify the first point where the process moves outside the agreed limit. Then make one controlled change, repeat the same test and compare sustained good output rather than a single successful pack.
Utilities and environmental trend
Log product temperature, room temperature, humidity, air pressure, vacuum, power and other critical utilities alongside the fault. Look for change over the run rather than one spot reading.
Application measure: For filling applications, include fill mass or volume, product temperature, viscosity, supply level or pressure, nozzle condition and finished-pack leakage.
Paste Fillers
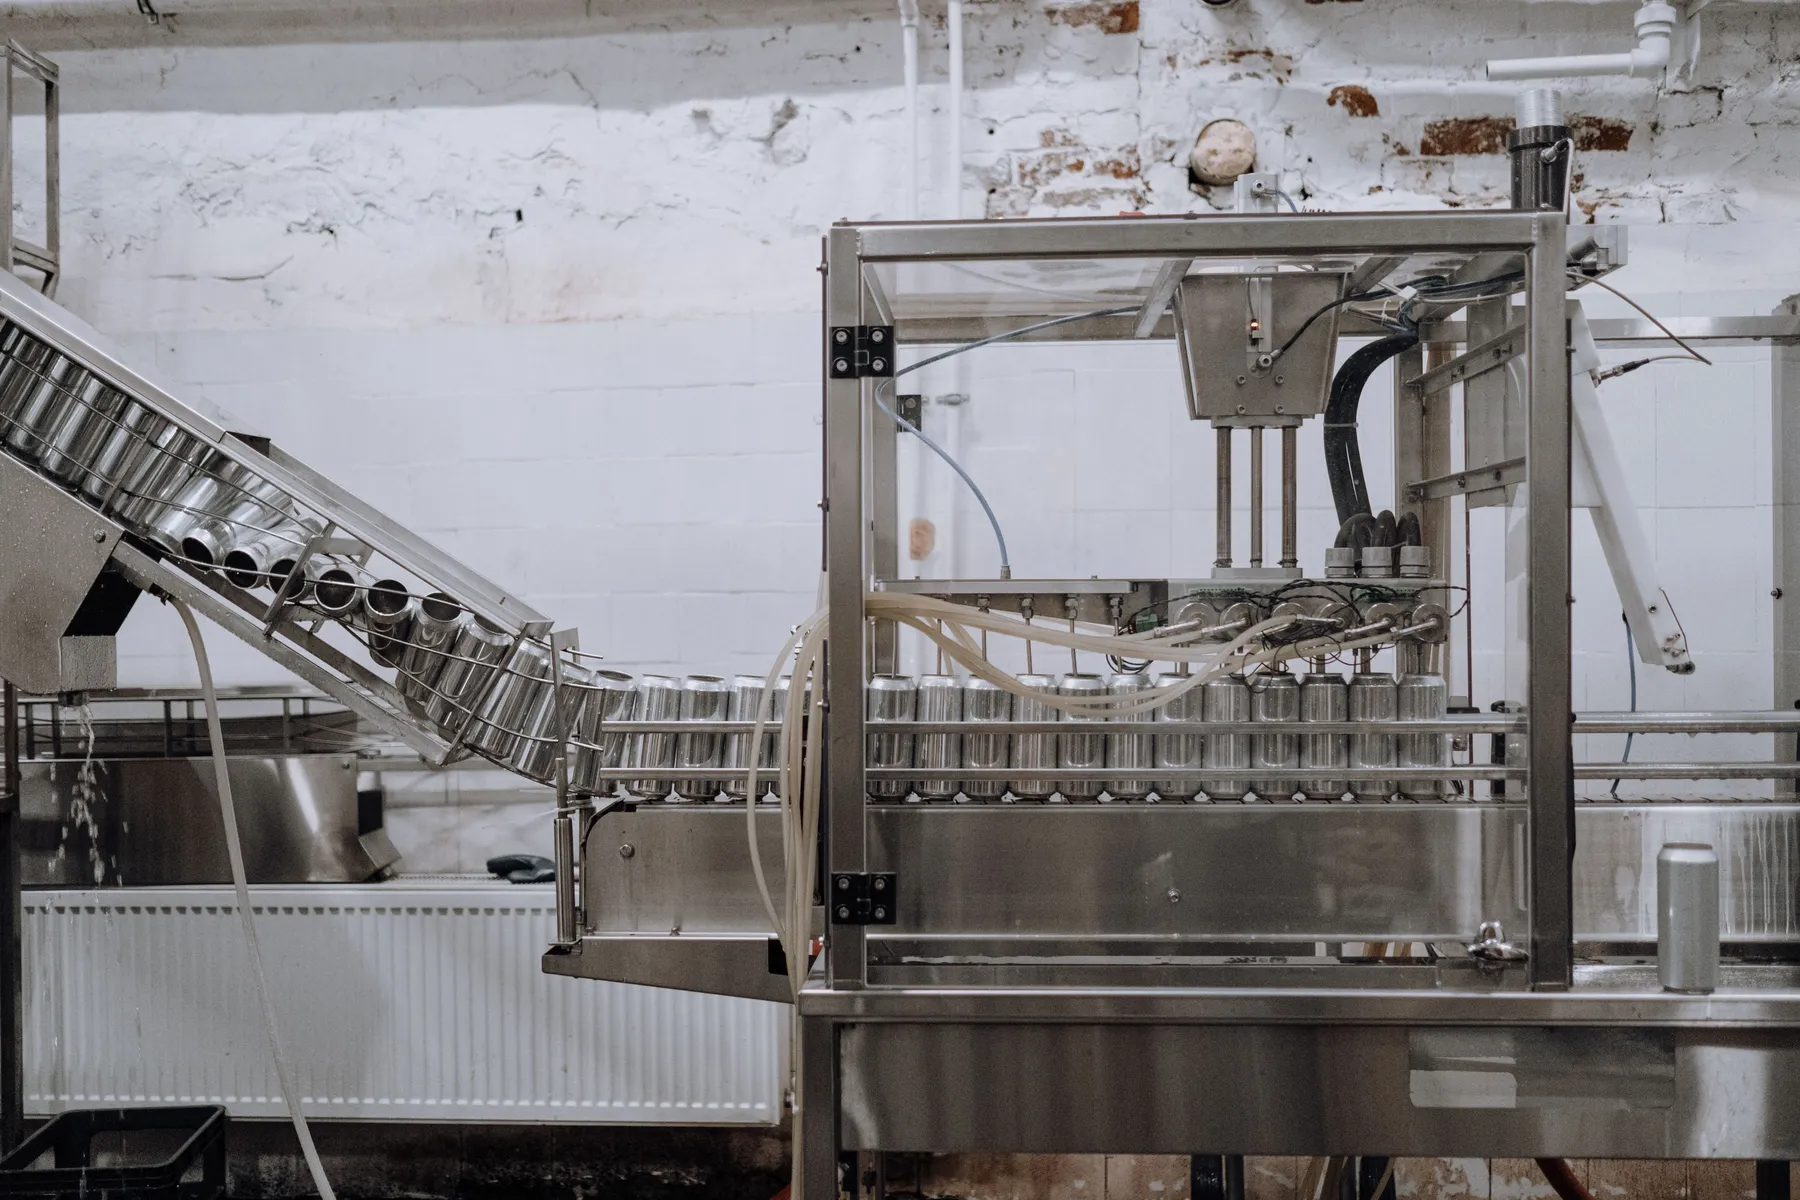
Filling sauces, creams, gels, pastes and adhesives.
What usually causes this?
- product viscosity or material stiffness changes with temperature
- humidity changes powder flow, static, labels or film
- air pressure, voltage, extraction or water quality varies under load
- room conditions are measured away from the actual process
- the equipment or method is not configured for a filling application where viscosity, aeration, temperature, supply conditions, nozzle control and product-contact compatibility affect dose and pack quality for mayonnaise. Product temperature, positive displacement, large product paths and clean nozzle shut-off are usually important.
Checks to make in order
- Record conditions beside the process
- Measure utilities while all connected equipment is running
- Compare product behaviour across the normal temperature range
- Check humidity, condensation, static and dust
- Verify compressed air, water, extraction and electrical quality
- Repeat performance at worst-case conditions
- Set monitoring and alarm limits where needed
How to decide the next step
Mayonnaise is a filling application where viscosity, aeration, temperature, supply conditions, nozzle control and product-contact compatibility affect dose and pack quality for mayonnaise. Product temperature, positive displacement, large product paths and clean nozzle shut-off are usually important. Use the measurements to decide whether the next action is a material or packaging change, a setting correction, a maintenance task, improved feeding or a different machinery principle.
If the process cannot achieve the required temperature, humidity and utilities result across the full product and pack range, compare the best-matched route against a written acceptance test. Include cleaning, changeover, operator work, rejects and recovery from normal stops.
What to include in your production brief
Supplying the information below makes it easier to distinguish a setup problem from a product, packaging, feeding, maintenance or machinery limitation:
- Product name, formulation and safety data
- Viscosity at the filling temperature
- Minimum and maximum fill quantity
- Required tolerance and measurement method
- Container dimensions and neck opening
- Required good packs per hour
- Samples that represent mayonnaise
- A short video of the present process and fault
Relevant solution websites
The first route is the primary match for this question. Final suitability must be confirmed with samples, output, site and acceptance information.
Related questions
 Liquid filling
What information is needed to specify a filler for mayonnaise?
Practical guidance for mayonnaise: capture samples, dimensions, output, acceptance tests and site constraints before buying.
Read the answer → Liquid filling
Why is filling mayonnaise too slow?
Practical guidance for mayonnaise: separate true machine speed from waiting, handling, replenishment and short stops.
Read the answer → Liquid filling
How do I reduce drips, giveaway and waste when filling mayonnaise?
Practical guidance for mayonnaise: reduce product loss, damaged packs, material waste and avoidable rejects.
Read the answer → Liquid filling
How do temperature and room conditions affect filling mineral water?
Practical guidance for mineral water: understand how the production environment changes product and machine behaviour.
Read the answer → Liquid filling
How do temperature and room conditions affect filling nail polish?
Practical guidance for nail polish: understand how the production environment changes product and machine behaviour.
Read the answer → Liquid filling
How do temperature and room conditions affect filling oat and plant drinks?
Practical guidance for oat and plant drinks: understand how the production environment changes product and machine behaviour.
Read the answer →